Brown Rice Applications, Buyers, and B2B Sourcing Opportunities
Brown Rice in the B2B Food Ingredient Market
Understanding Brown Rice as a Commercial Ingredient
Brown Rice is a rice product obtained after removing the outer husk while retaining much of the grain structure. In commercial food supply chains, this distinction makes Brown Rice different from conventional milled white rice and gives it relevance across food products where the characteristic grain appearance, texture, and composition are important. For B2B buyers, understanding the product form is an important first step when evaluating suppliers, specifications, and intended applications.
Brown Rice can serve both consumer-facing food manufacturers and processors that use rice as an input for further manufacturing. Its commercial value therefore extends beyond direct retail consumption. Buyers may source whole kernels, broken kernels, or specific grain types depending on the final product, processing route, packaging requirements, and target market.
Commercial Relevance for Food Manufacturers
The B2B relevance of Brown Rice comes from its ability to enter multiple stages of the food production chain. Manufacturers may use it as a finished grain ingredient, while processors can further mill or transform it into other rice-based ingredients. This creates opportunities for suppliers that can consistently meet requirements related to grain type, physical condition, packaging, and delivery.
For procurement teams, Brown Rice sourcing is consequently not limited to finding the lowest quoted price. Reliable supply, specification consistency, documentation, logistics capability, and responsiveness can all influence the suitability of a supplier. A structured procurement process helps buyers align the raw material with their manufacturing requirements.
Brown Rice Applications in Food Manufacturing
Direct Food Applications
Brown Rice is widely relevant to food products where rice is used as a principal grain ingredient. Food manufacturers can incorporate it into packaged grain products, ready-to-prepare meals, rice-based dishes, specialty food products, and other formulations where the identity and texture of the rice remain important. Application requirements can vary according to the desired cooking characteristics, grain appearance, and finished-product format.
For industrial buyers, the application determines many of the purchasing specifications. A manufacturer producing packaged Brown Rice may require consistent whole-kernel quality, while a processor making a secondary rice ingredient may place greater emphasis on milling performance and suitable raw-material characteristics. Procurement specifications should therefore be established around the final use rather than treating every Brown Rice requirement as identical.
Rice-Based Processed Foods
Brown Rice can also serve as an input for further processing into rice-based food ingredients and products. Processing may include milling, grinding, blending, or other transformations designed to produce a particular ingredient format. This creates demand from manufacturers that do not necessarily sell Brown Rice as a finished grain but instead incorporate it into broader product formulations.
For B2B suppliers, understanding these downstream applications can improve commercial positioning. Buyers in processed-food manufacturing may request information on grain type, physical characteristics, moisture-related requirements, packaging, and consistency between shipments. Suppliers that can communicate clearly about these characteristics can support more efficient qualification and procurement processes.
Brown Rice Processing and Product Development
Processing Requirements
Processing requirements depend strongly on the intended application. Brown Rice may enter a facility for cleaning, grading, packaging, milling, or additional transformation before reaching the final food product. Each stage can introduce quality considerations, making raw-material consistency an important part of manufacturing efficiency.
For processors, incoming Brown Rice should be assessed against agreed purchasing specifications before production. Factors such as kernel condition, grain type, foreign material, damaged kernels, broken kernels, and other physical characteristics may influence processing performance. Establishing clear specifications before shipment helps reduce uncertainty between suppliers and buyers.
Product Development Considerations
Food product developers may select Brown Rice based on the characteristics required by the final formulation. A product designed around recognizable whole grains can have different raw-material requirements from one that uses rice as an intermediate ingredient. The choice of Brown Rice therefore needs to reflect the product's manufacturing process as well as its intended market positioning.
B2B buyers can improve product-development efficiency by involving procurement and technical teams early in supplier discussions. Clear communication about grain form, intended application, packaging, expected volumes, and processing conditions allows suppliers to determine whether the proposed material is appropriate. This approach can also reduce the risk of sourcing a technically unsuitable specification.
Key Buyers of Brown Rice
Food Manufacturers
Food manufacturers represent an important buyer group for Brown Rice because the grain can be incorporated into a range of packaged and prepared food products. Their procurement requirements generally depend on production scale, product formulation, manufacturing equipment, packaging format, and market destination. Large-scale manufacturers may prioritize continuity of supply and standardized specifications across repeated shipments.
Smaller and specialized food producers may have more specific requirements concerning grain type, packaging quantities, or product characteristics. For both groups, supplier communication is essential because the same commodity can have different commercial requirements depending on the manufacturing process. A supplier capable of supporting specification discussions can therefore be valuable during the qualification stage.
Rice Processors and Distributors
Rice processors purchase Brown Rice when they require raw material for further milling or transformation. Distributors and commodity traders may also source Brown Rice for resale to food manufacturers, wholesalers, and regional buyers. These customers typically need commercially practical packaging, reliable shipment planning, and documentation that supports downstream transactions.
Distributor requirements can also vary according to destination market and customer portfolio. A distributor serving multiple food manufacturers may seek standardized Brown Rice specifications that can satisfy several applications. This makes flexibility, shipment consistency, and supplier responsiveness important considerations during vendor selection.
Quality and Specification Considerations
Physical Quality Parameters
Quality assessment is central to Brown Rice procurement because physical characteristics can influence both processing efficiency and finished-product consistency. Buyers may evaluate kernel condition, grain type, broken-kernel levels, damaged material, foreign material, and other characteristics according to the intended application. Specifications should be agreed before commercial purchase rather than assumed from the product name alone.
The exact acceptance criteria should reflect the buyer's manufacturing requirements and destination-market standards. Clear specification sheets can help procurement, quality-control, logistics, and supplier teams work from the same reference point. This is particularly important for recurring contracts where consistency between lots is a commercial requirement.
Documentation and Compliance
Food-industry buyers generally require appropriate documentation to support supplier qualification and internal quality procedures. Depending on the transaction, this may include product specifications, certificates of analysis, packaging information, origin details, and other documents requested by the buyer or destination market.
International sourcing can introduce additional documentation requirements because import rules and food standards differ between markets. Buyers should therefore confirm applicable requirements before shipment and communicate them clearly to suppliers. A documented compliance process can help reduce delays and prevent avoidable discrepancies during import, receiving, and quality inspection.
Brown Rice Sourcing and Procurement
Selecting a Suitable Supplier
Choosing a Brown Rice supplier involves evaluating more than product availability. Procurement teams may assess specification capability, supply capacity, shipment reliability, documentation, packaging options, communication, and the supplier's ability to maintain consistent quality. These factors become increasingly important when Brown Rice is a recurring production input rather than a one-time purchase.
A structured supplier-qualification process can begin with a technical specification and commercial inquiry. Buyers can then compare offered product characteristics, minimum order quantities, lead times, packaging formats, shipment terms, and documentation. This approach gives procurement teams a clearer basis for evaluating whether a supplier can support the complete purchasing requirement.
Bulk Purchasing Considerations
Bulk Brown Rice purchasing requires coordination between demand planning, supplier capacity, inventory management, and logistics. Buyers need to determine expected consumption, preferred shipment frequency, storage capability, and acceptable delivery windows before finalizing a supply arrangement. These factors can influence the practical cost of procurement even when the quoted unit price remains unchanged.
For international transactions, logistics planning becomes particularly important. Packaging, container utilization, port handling, transit time, customs documentation, and destination requirements should be considered alongside the product specification. A coordinated procurement plan can help manufacturers maintain material availability while reducing unnecessary supply-chain disruption.
Brown Rice Market and Supply Chain Considerations
Supply Chain Visibility
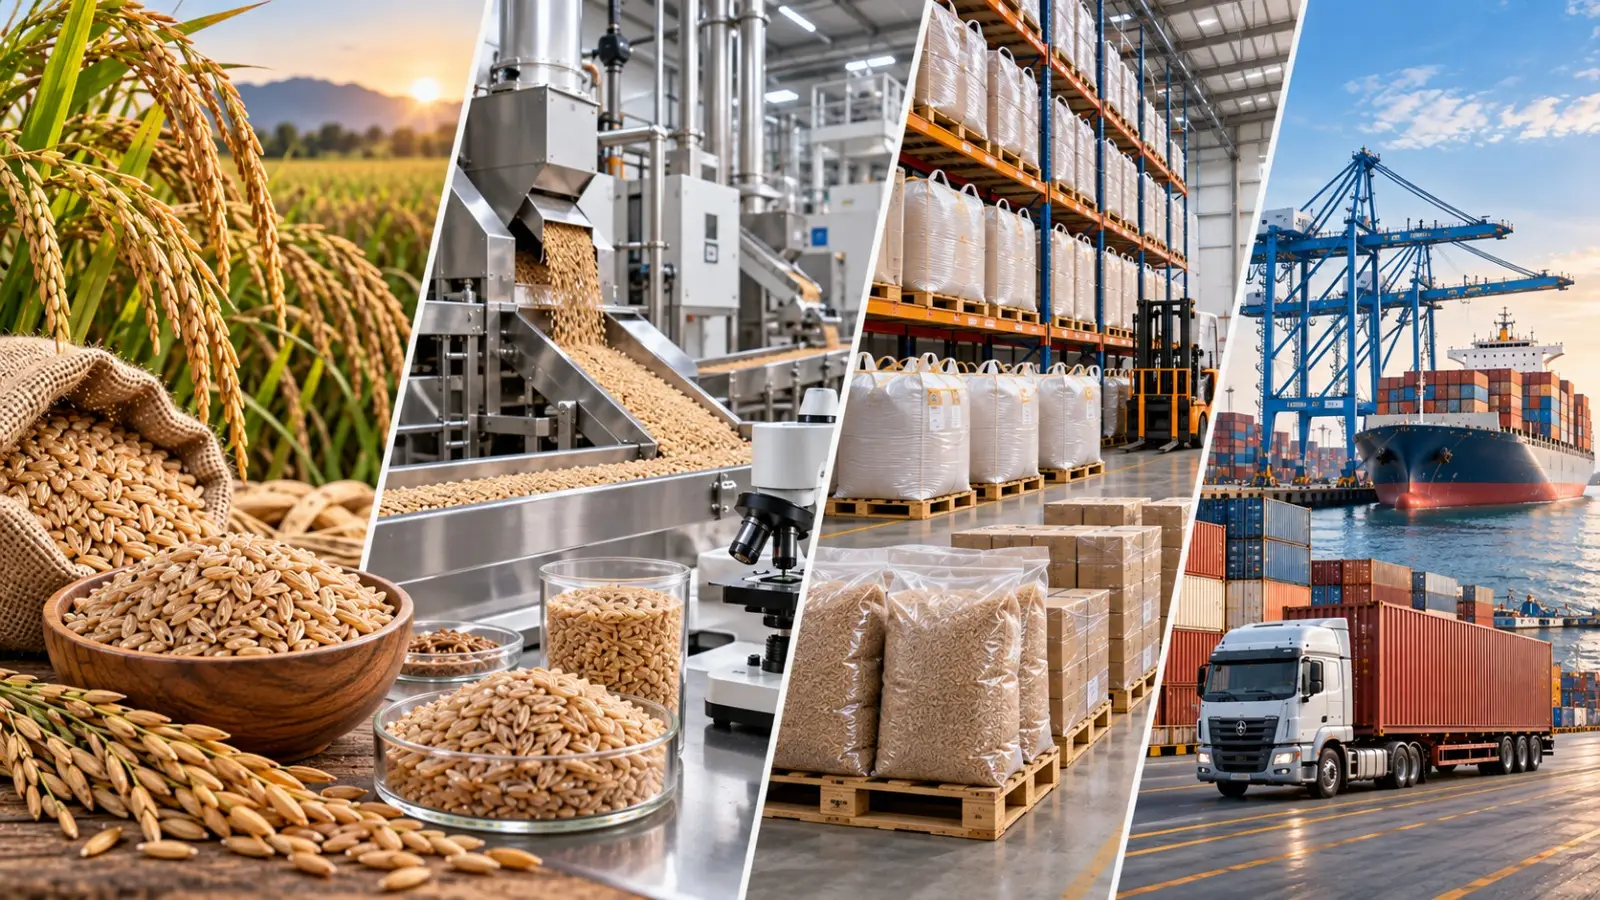
Brown Rice moves through a supply chain that can involve agricultural production, collection, drying, storage, processing, grading, packaging, warehousing, transportation, and international distribution. Each stage can affect the availability and consistency of the material delivered to industrial buyers. Supply-chain visibility is therefore valuable when planning recurring purchases.
B2B buyers can strengthen supply planning by discussing production capacity, available inventory, shipment schedules, packaging, and expected lead times with suppliers. This information helps procurement teams align purchasing decisions with production schedules. It also allows buyers to identify potential supply constraints before they affect manufacturing operations.
Market-Oriented Procurement
Market conditions can influence agricultural commodity procurement through changes in production, availability, logistics, demand, and regional trade flows. Buyers therefore benefit from monitoring supply conditions rather than relying exclusively on historical purchase prices. Market awareness can support more informed decisions regarding contract timing, inventory levels, and sourcing diversification.
For suppliers and distributors, market intelligence can similarly support better customer service. Understanding application demand and buyer requirements helps suppliers prepare appropriate product formats and commercial offers. A B2B marketplace can facilitate this process by connecting buyers and sellers and making product-sourcing discussions more accessible.
Building Reliable Brown Rice Supply Partnerships
Supplier-Buyer Communication
Long-term Brown Rice procurement depends on clear communication between the buyer and supplier. Product specifications, target volumes, packaging, shipment schedules, quality documentation, and commercial terms should be discussed before the transaction is finalized. Clear communication reduces ambiguity and helps both sides plan production and logistics more effectively.
Supplier relationships can become more efficient when procurement teams establish repeatable processes for inquiries, samples, approvals, purchase orders, inspections, and shipment documentation. This is particularly useful for manufacturers purchasing Brown Rice on a recurring basis. A consistent workflow can shorten procurement cycles while maintaining technical and commercial controls.
B2B Marketplace Opportunities
A B2B marketplace can provide a practical sourcing environment for buyers looking to identify Brown Rice suppliers, compare product offerings, and initiate commercial discussions. For suppliers, marketplace visibility can create opportunities to reach food manufacturers, distributors, processors, and other professional buyers seeking agricultural ingredients.
For Tradeasia, Chemtradeasia, and Tradechem Marketplace, Brown Rice represents a product category where agricultural sourcing and food-industry procurement intersect. Presenting product information around applications, buyer requirements, quality expectations, and sourcing considerations can help professional users understand where the material fits within their supply chain.
Conclusion: Brown Rice Opportunities for B2B Buyers
Procurement Priorities
Brown Rice offers a commercially relevant raw-material option for food manufacturers, rice processors, distributors, and other professional buyers. Its applications can range from direct grain products to further processed rice-based ingredients, creating different specification requirements across the supply chain. Buyers should align product selection with their manufacturing process and final application.
A reliable sourcing strategy should combine product specifications with supplier capability, documentation, logistics, quality control, and supply continuity. Establishing these requirements before purchase can help procurement teams identify suitable suppliers and create more predictable purchasing processes. For recurring demand, supplier qualification and specification consistency become particularly important.
Connecting Buyers with Supply Opportunities
The commercial opportunity for Brown Rice extends across agricultural production, food manufacturing, processing, distribution, and international trade. Buyers seeking dependable supply can benefit from evaluating suppliers according to both technical and commercial requirements rather than focusing on price alone. Suppliers, meanwhile, can improve their market reach by clearly presenting product specifications and application relevance.
Through a professional B2B marketplace environment, Brown Rice buyers and suppliers can establish connections around practical sourcing requirements. Tradeasia, Chemtradeasia, and Tradechem Marketplace can position Brown Rice within a broader food-ingredient and agricultural sourcing ecosystem, helping procurement teams explore supply opportunities based on application, quality, volume, and market needs.
Sources
https://www.ams.usda.gov
https://www.fao.org
https://www.fao.org
Leave a Comment