Black Rice Supply Chain Overview
Understanding Black Rice as a B2B Ingredient
Black Rice, scientifically associated with Oryza sativa, is a pigmented rice variety distinguished by its dark outer grain layer. Research reviews identify anthocyanins, phenolic compounds, dietary fibre, essential amino acids, γ-oryzanols, tocopherols, tocotrienols, and phytosterols among the compounds associated with black rice. These characteristics have supported interest in black rice for food and beverage development beyond conventional rice applications.
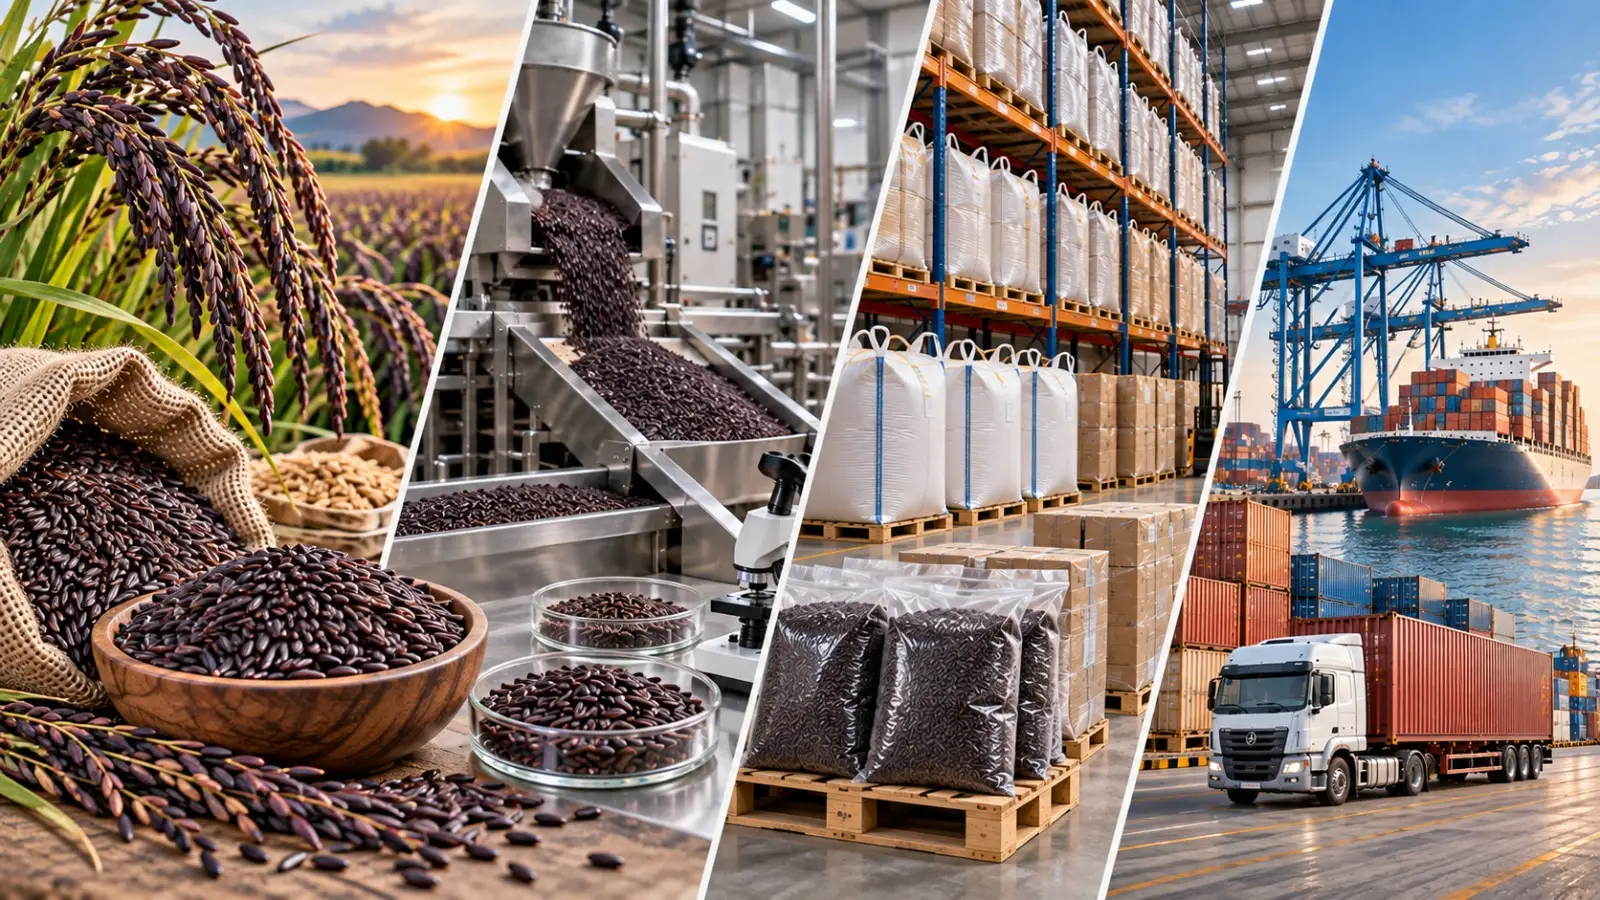
From a B2B supply-chain perspective, Black Rice is more than an agricultural commodity because its commercial value can depend on cultivar, grain quality, post-harvest handling, processing format, and consistency between shipments. Buyers may source whole grain, milled grain, flour, or other processed formats depending on the intended application. For international procurement teams, understanding how the product moves from cultivation through processing and distribution is therefore important when evaluating suppliers.
Why Supply-Chain Management Matters
The quality of Black Rice can be influenced by activities occurring throughout the chain, including harvesting, drying, storage, milling, packaging, transportation, and final processing. Research on black rice has specifically examined how drying, storage, cooking, extrusion, and other processes can alter phenolic compounds and anthocyanins.
For buyers, a reliable supply chain should connect agricultural production with controlled post-harvest operations and documented quality management. This creates greater visibility over product specifications, batch consistency, packaging, shelf-life expectations, and shipment preparation. A B2B marketplace can support this process by connecting qualified buyers with suppliers while making sourcing requirements clearer from the beginning.
Black Rice Production and Raw Material Sourcing
Agricultural Supply and Cultivar Selection
The first stage of the Black Rice supply chain is agricultural production. Different pigmented rice cultivars can vary in grain characteristics, colour intensity, composition, yield, and processing performance. Consequently, commercial buyers should define the required product format and quality parameters before entering into large-volume procurement arrangements.
Sourcing begins with identifying suitable production regions and suppliers capable of maintaining consistent agricultural and post-harvest practices. For B2B procurement, the supplier relationship can influence availability, batch uniformity, documentation, and the ability to meet recurring order volumes. Long-term sourcing programs can therefore require more than simply comparing individual shipment prices.
Managing Raw Grain Consistency
Raw grain consistency is an important consideration because agricultural commodities naturally experience variation between harvests. Moisture, foreign material, damaged grains, grain size, colour, and other quality parameters can affect downstream processing and the suitability of the material for different food applications.
A structured sourcing program should connect the buyer's product specification with supplier quality documentation. Where Black Rice is intended for food manufacturing, procurement teams may also need to evaluate food-safety controls, traceability procedures, packaging standards, and applicable regulatory requirements in the destination market. Codex maintains an international Standard for Rice, CXS 198-1995, which provides a relevant international reference for rice quality considerations.
Post-Harvest Handling and Processing
Drying and Moisture Management
Post-harvest handling is a critical stage in the Black Rice supply chain. Freshly harvested grain contains relatively high moisture and requires appropriate drying before extended storage. Research reviewing black rice processing notes that drying and storage are important for maintaining grain safety, shelf life, and quality, while processing conditions can also influence bioactive compounds.
For commercial buyers, moisture management has direct supply-chain implications because inadequate drying can increase storage risks, while aggressive drying conditions can affect product characteristics. Research has reported changes in phenolic compounds and other bioactive components under different drying conditions, reinforcing the importance of controlled post-harvest practices.
Milling and Value-Added Processing
Milling converts harvested rice into a commercially usable format and can significantly influence the final product specification. Depending on the market, Black Rice may be supplied as whole grain, milled rice, broken rice, flour, or an ingredient incorporated into further processed foods. Each format creates different requirements for processing equipment, packaging, handling, and buyer specifications.
Further processing can also affect the functional characteristics that make pigmented rice commercially interesting. Reviews have documented changes in anthocyanins and phenolic compounds following cooking, drying, extrusion, and other processing methods. Therefore, processors should match the selected Black Rice format and processing conditions with the characteristics required by the finished product.
Quality Control and Specification Management
Key Quality Considerations
Quality control for Black Rice should begin with a clearly defined commercial specification. Depending on the intended application and destination market, buyers may evaluate parameters such as grain appearance, moisture, foreign matter, broken grains, cleanliness, packaging condition, and microbiological or contaminant requirements. The exact specification should be established between buyer and supplier before shipment.
Quality consistency is particularly important for food manufacturers purchasing Black Rice on a recurring basis. Variations in raw material characteristics can affect milling yields, flour performance, cooking behaviour, colour, texture, and finished-product consistency. Supplier qualification can therefore form an important part of the procurement process rather than being treated as a one-time purchasing decision.
Documentation and Traceability
Documentation provides buyers with greater visibility across the supply chain. Depending on the transaction, relevant commercial and technical documentation may include product specifications, certificates of analysis, batch information, origin documentation, packaging details, and other compliance records required by the buyer or destination market.
Traceability is also relevant when Black Rice moves through multiple supply-chain stages. Clear identification of lots and batches can help connect agricultural production with processing, storage, shipment, and delivery records. For international B2B sourcing, this documentation can support communication between procurement, quality assurance, logistics, regulatory, and receiving teams.
Storage and Logistics Considerations
Maintaining Product Quality During Storage
Storage conditions are an important part of Black Rice supply-chain management because quality does not depend solely on production and processing. Research has shown that storage conditions and duration can influence the levels of phenolic compounds and other bioactive components in black rice.
Commercial storage should therefore focus on protecting the product from conditions that may contribute to deterioration, contamination, pest activity, or undesirable changes in quality. Appropriate warehouse practices, packaging, moisture management, stock rotation, and lot identification can help maintain product integrity while inventory is held before domestic distribution or export.
International Transportation
Transportation adds another layer of supply-chain control, particularly when Black Rice is traded internationally. Export shipments may involve inland transport, consolidation, container loading, port handling, ocean freight, customs clearance, and final delivery to a processing facility or distribution warehouse.
B2B buyers should align logistics planning with order volume, packaging format, destination requirements, delivery schedules, and product shelf-life considerations. Clear shipping documentation and coordination between suppliers, freight providers, customs teams, and receiving facilities can reduce avoidable delays and support predictable procurement planning.
Industrial Applications and Buyer Requirements
Food and Beverage Applications
Black Rice can be incorporated into a range of food and beverage products. Published research has examined its use in functional foods, cereals, bakery-related products, beverages, pasta, and other processed food formats. Its pigmentation and naturally occurring bioactive compounds can provide differentiation for product developers seeking distinctive grain-based ingredients.
For industrial food manufacturers, application suitability depends on more than nutritional composition. Processing behaviour, particle size, moisture, colour, flavour, cooking characteristics, and compatibility with other ingredients can all influence commercial performance. Buyers therefore need to select the appropriate Black Rice grade or processed format for the intended formulation.
Requirements of Different B2B Buyers
Food manufacturers may purchase Black Rice for direct grain products or as an input for further processing, while ingredient processors may require specific milling or flour characteristics. Distributors and wholesalers, meanwhile, may place greater emphasis on packaging formats, shipment volumes, documentation, availability, and consistent supply.
These different buyer profiles create different sourcing requirements. A bakery ingredient buyer may focus on flour functionality, whereas a cereal producer may require specific grain characteristics. Procurement teams can improve supplier matching by communicating the intended application, required specification, target volume, packaging format, destination, and delivery schedule before requesting commercial quotations.
Global Sourcing and B2B Procurement
Supplier Evaluation
Selecting a Black Rice supplier involves evaluating both product quality and supply capability. Buyers can examine production and processing capacity, quality-control systems, product specifications, documentation, packaging capabilities, export experience, and the supplier's ability to maintain consistent availability.
Price remains a commercial consideration, but it should be evaluated alongside total procurement requirements. Differences in product specification, packaging, minimum order quantity, logistics, documentation, lead time, and quality consistency can affect the actual landed procurement cost. A structured supplier evaluation can help procurement teams compare quotations on a like-for-like basis.
B2B Marketplace Sourcing
A B2B marketplace can simplify supplier discovery by bringing product information, sourcing requirements, and commercial communication into a more structured environment. For Black Rice buyers, this can help connect demand for bulk quantities with suppliers capable of supporting food manufacturing, distribution, and international trade requirements.
For suppliers, marketplace visibility can provide access to buyers searching for specialty rice and food ingredients across different markets. Clear product descriptions, technical information, packaging details, supply capabilities, and commercial terms can make supplier profiles more useful to professional procurement teams. The objective is to create a more transparent connection between product availability and verified commercial demand.
Supply Chain Outlook and Conclusion
Building a More Resilient Black Rice Supply Chain
A resilient Black Rice supply chain depends on coordination between agricultural producers, processors, quality-control teams, warehouses, logistics providers, distributors, and final industrial buyers. Each stage can influence the consistency and commercial usability of the product delivered to the customer.
Research on Black Rice demonstrates that drying, storage, and processing can affect its bioactive composition, meaning supply-chain management is relevant not only to physical product preservation but also to the characteristics valued by food manufacturers.
Procurement Priorities for B2B Buyers
For procurement teams, an effective sourcing strategy should begin with a precise product specification and then evaluate supplier capability, quality documentation, processing controls, packaging, logistics, and recurring availability. This approach can help buyers distinguish between a one-time commodity purchase and a sustainable industrial sourcing relationship.
Black Rice therefore represents a specialty agricultural ingredient where supply-chain visibility can support commercial decision-making from origin to final delivery. With appropriate supplier qualification, quality management, storage controls, and logistics planning, B2B buyers can develop sourcing programs aligned with food manufacturing and ingredient-distribution requirements.
Sources
https://www.fao.org
https://pubmed.ncbi.nlm.nih.gov
https://pubmed.ncbi.nlm.nih.gov
Leave a Comment