Black Rice Applications and B2B Buyers: Sourcing Guide
Black Rice Overview and Commercial Positioning
Understanding Black Rice as a Specialty Grain
Black Rice is a pigmented variety of Oryza sativa that has developed a distinct position within specialty grains and food ingredients. Unlike conventional white rice, its dark coloration is associated with naturally occurring pigments and bioactive compounds, particularly anthocyanins and other phenolic compounds. Research reviews identify black rice as a source of dietary fiber, essential amino acids, γ-oryzanols, tocopherols, tocotrienols, phytosterols, minerals, and other naturally occurring components of interest to food developers.
From a B2B perspective, Black Rice can be considered both a staple grain and a specialty ingredient. Its visual appearance, nutritional profile, and potential use in differentiated food formulations allow manufacturers to develop products positioned around whole grains, specialty cereals, functional foods, and premium food concepts. This gives distributors and ingredient traders several potential customer segments beyond conventional rice procurement.
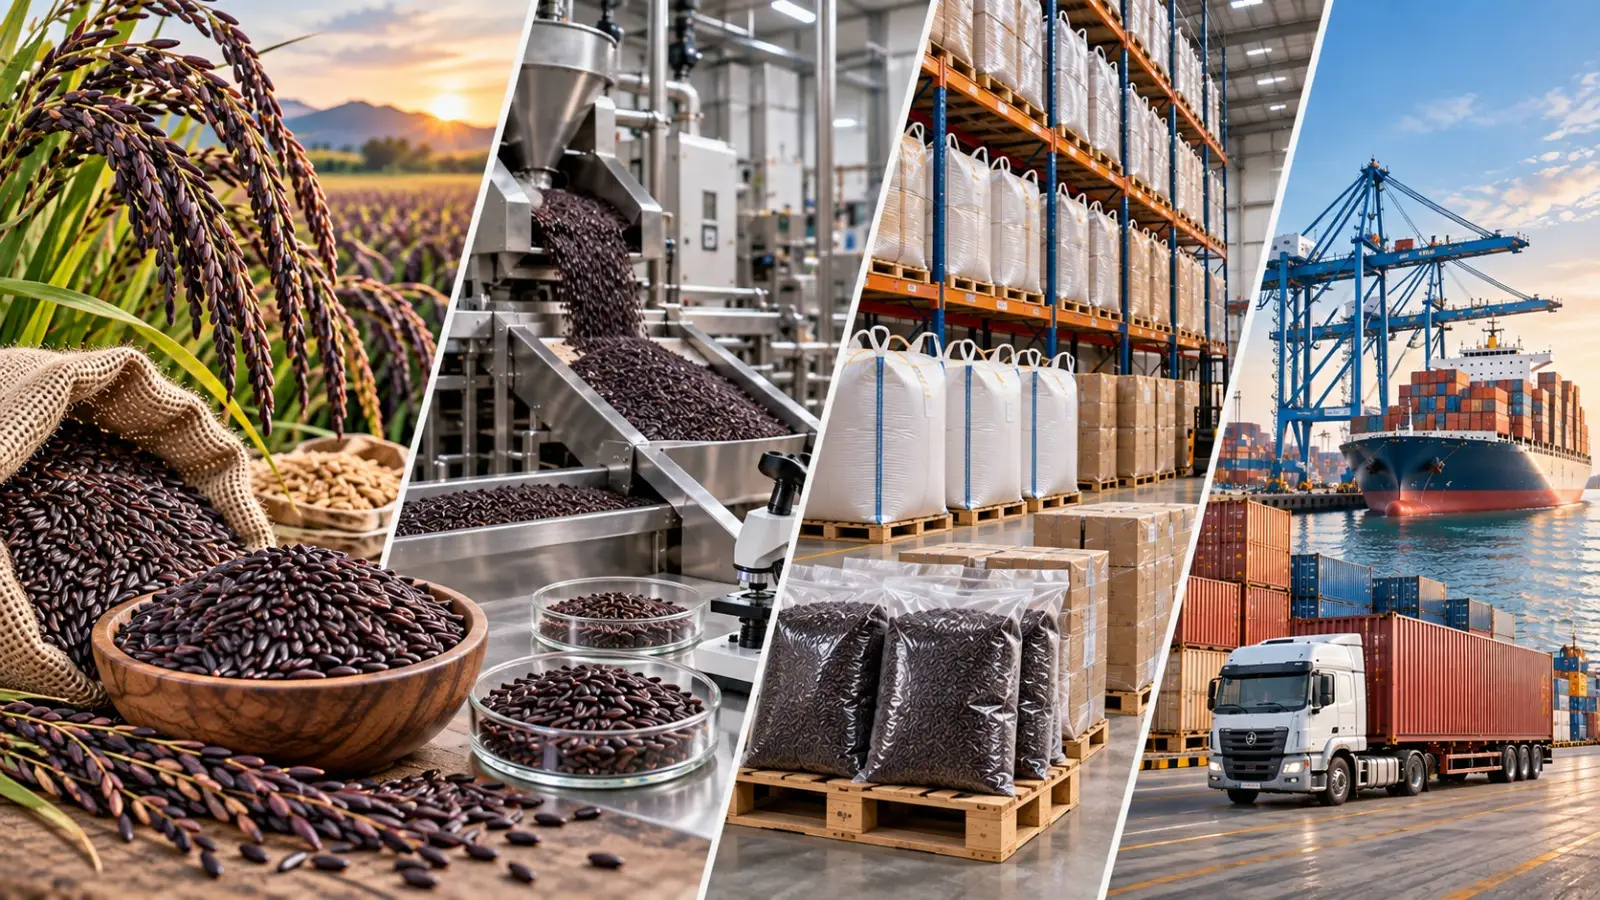
The commercial value of Black Rice is closely connected to how it is processed, presented, packaged, and incorporated into finished products. Buyers may require whole kernels, milled material, flour, or other processed forms depending on their manufacturing process. Consequently, sourcing discussions should focus not only on the commodity itself but also on specification, processing format, consistency, packaging, documentation, and intended application.
For international B2B trade, product identity and quality specifications remain important considerations. The Codex Standard for Rice, CXS 198-1995, covers husked, milled, and parboiled rice for direct human consumption and provides an international reference point for rice quality and handling. For Black Rice buyers, the applicable specification should therefore be clearly defined according to the product form and destination-market requirements.
Key Applications of Black Rice
Black Rice for Food Manufacturing
Black Rice can be incorporated into a broad range of food products where manufacturers want a distinctive grain ingredient, characteristic dark appearance, or specialty nutritional profile. Research literature identifies applications in functional foods, gluten-free cereals, beverages, and other food products. This creates opportunities for processors developing differentiated products rather than competing solely within conventional white-rice categories.
In cereal manufacturing, Black Rice may be used in whole-grain products, breakfast cereals, grain mixes, and specialty rice formulations. Its pigmentation can provide a naturally distinctive visual characteristic, while its grain structure makes it suitable for products in which rice remains a recognizable component. Manufacturers can also evaluate Black Rice flour for applications where a milled ingredient is more compatible with existing production systems.
Bakery and snack manufacturers represent another potential buyer group. Black Rice ingredients can be incorporated into selected baked products, crackers, snack formulations, grain bars, and specialty flour blends, subject to formulation requirements. Research on black and purple rice anthocyanins has also examined their incorporation into food products such as bread and beverages, highlighting the broader application potential of rice-derived bioactive ingredients.
Beverage and ready-to-eat food developers can also evaluate Black Rice for specialty product concepts. Depending on processing and formulation, the grain may be incorporated into rice-based beverages, cereal beverages, desserts, prepared foods, and other products. For B2B procurement, the appropriate form of Black Rice should be selected according to processing equipment, particle-size requirements, cooking characteristics, flavor profile, and finished-product specifications.
Black Rice in Functional and Specialty Foods
Functional Food Development
Black Rice has attracted research interest because of its naturally occurring bioactive compounds, particularly anthocyanins and phenolic compounds. A review published in 2017 described black rice as a source of anthocyanins, other phenolics, and terpenoids and discussed its potential role in functional-food development. For commercial food manufacturers, this research supports continued interest in Black Rice as a specialty raw material, while product claims must still comply with the regulations applicable to the target market.
The functional-food opportunity is particularly relevant to manufacturers developing products around whole grains and naturally occurring food components. Black Rice can be considered for cereals, grain blends, nutritional foods, specialty snacks, and other products where the ingredient's composition and appearance contribute to product differentiation. However, procurement teams should distinguish between the documented composition of an ingredient and specific health claims that may require regulatory substantiation.
Black Rice by-products can also be commercially relevant. Recent research has examined anthocyanin-rich extracts derived from Black Rice and its by-products, including their potential applications in functional foods, supplements, and natural-colorant development. The same review emphasizes that additional clinical research is required before potential biological effects can be established for human-health claims. This distinction is important for responsible B2B marketing and product development.
For ingredient buyers, the opportunity therefore extends beyond selling or purchasing whole Black Rice kernels. Depending on capabilities and regulatory requirements, processors may explore flour, bran-related materials, or extracts as separate ingredient categories. The commercial specification should clearly identify the form being purchased, intended application, analytical requirements, and permitted claims so that product development remains aligned with regulatory and quality expectations.
Processing and Quality Considerations
Processing Effects on Product Characteristics
Processing is a major consideration when sourcing Black Rice because drying, storage, cooking, milling, and other treatments can affect its physical and chemical characteristics. A 2023 review reported that processing and storage conditions can influence bioactive compounds in Black Rice, including anthocyanins, phenolic compounds, γ-oryzanols, and other components. This makes processing history relevant when buyers compare products from different suppliers.
Industrial processing can influence the characteristics that matter to food manufacturers, including color, aroma, texture, cooking behavior, particle size, and the retention of selected bioactive compounds. Research published in Foods similarly notes that drying, storage, cooking, and extrusion can affect phytochemical content and antioxidant capacity in Black-Rice-based foods. Procurement teams should therefore evaluate the ingredient according to its actual application rather than relying only on its generic product name.
Storage conditions are another important part of quality management. Research on Thai Black Rice found that drying methods, storage temperature, storage duration, and packaging affected selected bioactive compounds and aroma-related characteristics. For international trade, appropriate packaging and storage controls can therefore help preserve product characteristics during warehousing and transportation.
Quality documentation should be matched to the buyer's intended use and destination market. Depending on the application, buyers may request specifications covering moisture, foreign matter, broken kernels, microbiological parameters, contaminants, pesticide residues, packaging, shelf life, and other quality indicators. International rice standards such as Codex CXS 198-1995 provide a useful reference framework, while individual markets and customers may impose additional requirements.
Black Rice Buyers and Procurement Requirements
Food Manufacturers as Core Buyers
Food manufacturers are an important buyer segment because Black Rice can be incorporated into multiple product categories. Cereal producers may purchase whole grain or processed forms, while bakery, snack, beverage, and specialty-food manufacturers may have different requirements for flour, grain size, cooking properties, or processing compatibility. The purchasing specification should therefore be developed around the finished product rather than treating Black Rice as a one-size-fits-all ingredient.
Ingredient distributors are another relevant B2B customer group. Distributors typically need dependable product specifications, consistent supply, suitable packaging, documentation, and commercially practical minimum order quantities. Their requirements may also include multiple packaging formats to serve food manufacturers of different sizes and applications.
Private-label and specialty-food companies can represent additional demand. These businesses may use Black Rice as part of premium, whole-grain, functional, gluten-free, or visually distinctive product concepts. For these buyers, consistency between batches can be particularly important because changes in grain appearance, cooking behavior, or ingredient quality can affect finished-product performance.
Procurement teams should also distinguish between spot purchasing and long-term sourcing. A single shipment may satisfy a short production requirement, while recurring manufacturing programs require greater attention to supplier capacity, quality consistency, lead times, logistics, documentation, and contingency planning. Establishing these requirements early can make supplier evaluation more efficient and reduce avoidable procurement risk.
Black Rice Sourcing and Supply Chain Considerations
Supplier Evaluation and Specification Management
B2B Black Rice sourcing should begin with a clear product specification. Buyers should define the desired form, grade, physical characteristics, packaging format, intended application, expected annual or shipment volume, destination, and relevant regulatory requirements. A detailed specification allows suppliers to quote comparable products and helps procurement teams avoid comparing materials that are commercially or technically different.
Supplier qualification should also consider the ability to maintain consistent quality across multiple shipments. Black Rice is an agricultural product, so characteristics can vary according to variety, cultivation conditions, post-harvest handling, processing, and storage. Buyers may therefore request certificates of analysis, product specifications, traceability information, food-safety documentation, and representative samples before moving into larger-volume procurement.
Logistics planning is equally important for international trade. Packaging should protect the grain from moisture, contamination, physical damage, and unsuitable storage conditions. Warehousing and transportation arrangements should be appropriate for the product's shelf-life requirements and destination climate. This is particularly relevant when Black Rice is transported over long distances or passes through multiple storage and distribution points.
A structured sourcing process can help buyers manage both commercial and technical requirements. Instead of evaluating price alone, procurement teams can compare specification compliance, documentation, packaging, minimum order quantity, lead time, supply continuity, and logistics options. For marketplace-based B2B sourcing, this approach helps connect product requirements with suppliers that are better aligned with the intended application.
Market Opportunities and Commercial Demand
Specialty Grain and Functional Food Demand
The commercial opportunity for Black Rice is linked to the broader development of specialty grains, functional foods, whole-grain products, and differentiated food formulations. Academic reviews have documented growing research interest in Black Rice because of its nutritional composition and bioactive compounds, as well as its applications in functional foods and beverages. This provides a technical foundation for continued product-development activity.
Food manufacturers are increasingly able to use differentiated grains as part of product positioning, but commercial success depends on practical manufacturing requirements. Black Rice must perform consistently within the production process, meet applicable food-safety specifications, and remain commercially viable at the required scale. Buyers therefore need both market awareness and technical procurement criteria when assessing potential supply opportunities.
Product diversification creates another opportunity. Manufacturers can evaluate Black Rice across cereals, bakery products, snacks, beverages, ready-to-eat foods, grain blends, and specialty food products. Research has also investigated Black Rice and its by-products for anthocyanin-rich ingredients and natural-colorant applications. These developments broaden the potential customer base beyond traditional rice consumption.
For suppliers and distributors, this diversification means that buyer requirements can differ substantially between applications. A cereal manufacturer may prioritize kernel integrity and cooking behavior, while a flour processor may focus on particle size and milling performance. Extract developers may instead require standardized bioactive composition and additional analytical documentation. Understanding these differences is essential for targeted B2B market development.
How B2B Buyers Can Source Black Rice
Building an Efficient Procurement Process
A practical Black Rice sourcing process begins by defining the exact product requirement. Buyers should specify whether they need whole kernels, husked rice, milled rice, flour, bran-related material, or another processed form. They should also identify the intended food application, required quantity, packaging preference, delivery location, and relevant quality and regulatory criteria before requesting quotations.
Supplier inquiries should include sufficient technical information to generate meaningful commercial offers. A buyer may request product specifications, certificates of analysis, sample availability, packaging details, shelf-life information, origin or traceability documentation, minimum order quantity, production capacity, lead time, and shipping options. This enables procurement teams to compare suppliers on a consistent basis.
Sampling and validation can be especially important for new suppliers. Food manufacturers may evaluate cooking performance, color, flavor, texture, milling behavior, microbiological quality, and other application-specific characteristics before approving a material. Where the product is intended for a functional-food or specialty formulation, buyers may also require additional analytical information relating to relevant compounds or processing characteristics.
B2B marketplaces can support this process by connecting buyers with suppliers and distributors across different markets. For Black Rice, the most useful sourcing approach is one that combines commercial information with technical specifications, application requirements, and supply capabilities. This allows procurement teams to move from general product discovery toward qualified sourcing decisions based on their own operational requirements.
Conclusion: Building Reliable Black Rice Supply
From Specialty Grain to B2B Ingredient Opportunity
Black Rice occupies a distinctive position between conventional grain supply and specialty food ingredients. Its naturally pigmented appearance, nutritional composition, and documented presence of anthocyanins and other bioactive compounds have generated interest across food science and product development. For B2B buyers, these characteristics create opportunities across specialty grains, functional foods, cereals, snacks, beverages, bakery products, and other food applications.
The most relevant buyers include food manufacturers, ingredient distributors, specialty-food producers, cereal companies, bakery and snack manufacturers, and businesses developing functional-food concepts. Each buyer category can require a different product format and quality specification. As a result, supplier selection should be based on application fit, documentation, consistency, logistics, and commercial terms rather than product naming alone.
Reliable sourcing also depends on understanding processing and storage. Research indicates that processing, drying, storage, and packaging can influence the characteristics and bioactive components of Black Rice. Buyers should therefore include handling and storage requirements in their procurement specifications, particularly when sourcing internationally or purchasing larger commercial volumes.
For Tradeasia / Chemtradeasia / Tradechem Marketplace, Black Rice represents a B2B sourcing category that connects agricultural production with food manufacturing and specialty ingredient demand. A structured approach to specifications, supplier qualification, samples, documentation, logistics, and application requirements can help buyers develop dependable supply relationships while enabling suppliers to reach manufacturers seeking differentiated rice-based ingredients.
Sources
https://www.fao.org
https://pubmed.ncbi.nlm.nih.gov
https://pubmed.ncbi.nlm.nih.gov
Leave a Comment